
Whether you’re assembling machinery, working on an engine block, or designing a mold, threaded holes are a fundamental part of mechanical assemblies. These internal threads allow screws, bolts, and fasteners to hold components securely, ensuring both strength and stability. While creating a threaded hole might seem straightforward, achieving high-quality threads requires proper planning, tooling, and technique. This guide explores the essentials of threaded hole machining, from types and methods to best practices and troubleshooting tips
What Is a Threaded Hole?
A threaded hole is simply a drilled cavity in a workpiece with internal threads, allowing fasteners to engage securely. It is sometimes referred to as a tapped hole, but the term threaded hole also includes other methods of forming threads, such as thread milling or thread forming.

It’s important to distinguish threaded holes from clearance holes, which are simply larger drilled holes that allow a screw or bolt to pass through freely. Threaded holes typically adhere to standards such as ISO, ANSI, UNC, and UNF, which define dimensions, pitch, and tolerances — ensuring compatibility across different fasteners and components.
Types of Threaded Holes
Through Hole vs. Blind Hole
- Through holes pass entirely through the material and are easier to tap.
- Blind holes stop inside the workpiece, requiring precise depth control to avoid incomplete threads.
Tapered Threads vs. Straight Threads
- Tapered threads are used in sealing applications, like pipe fittings.
- Straight threads are used for general fastening, where maximum strength and precision are essential.
Metric vs. Imperial Threads
- Metric threads follow international standards and are widely used in machinery.
- Imperial threads (inch-based) remain common in certain industries, especially in North America.
Methods for Internal Threading
- Tapping: Using hand taps or CNC tapping machines to cut threads directly.
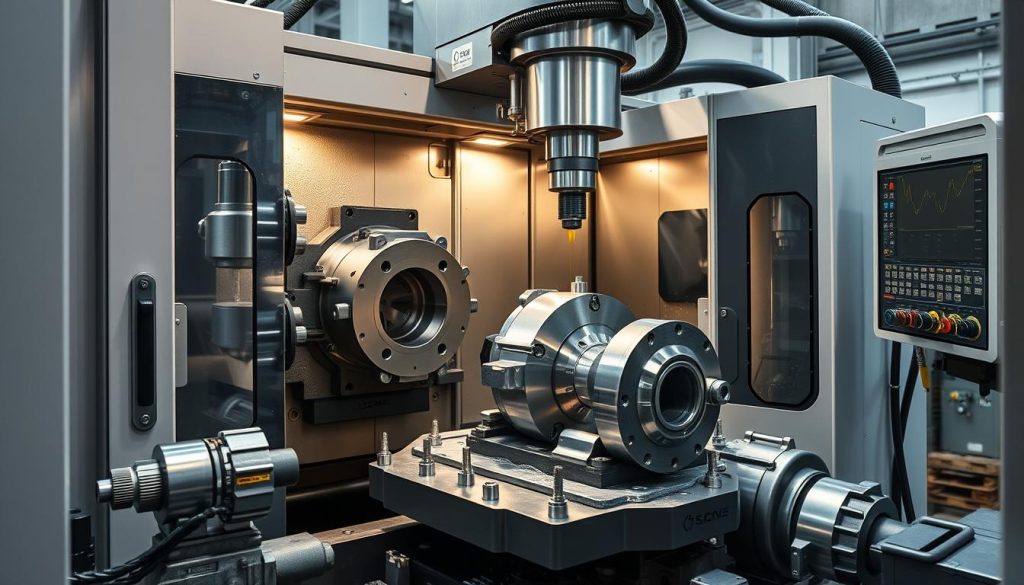
- Thread Milling: CNC machines carve threads along a helical path, offering high accuracy and flexibility.
- Thread Forming: Deforms material instead of cutting it, creating strong threads in softer metals like aluminum or copper.
How Threaded Holes Are Machined
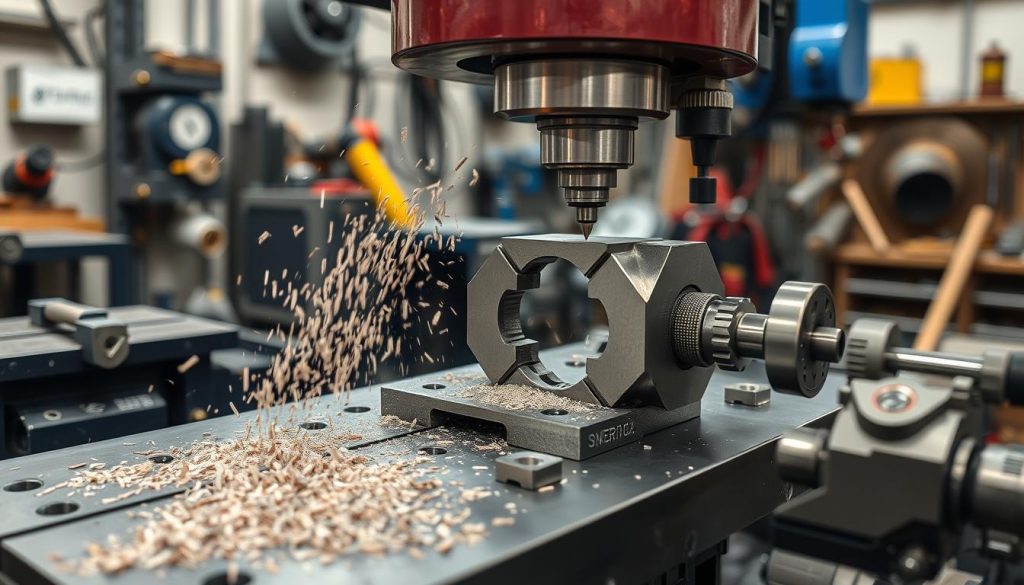
- Drill the Pilot Hole
The first step is drilling a pilot hole, sized according to the intended thread. Using a tap drill size chart ensures the correct diameter — too small, and the tap can break; too large, and threads may be weak or loose.
- Cutting Threads
- Tapping: A traditional method where a tap cuts the internal threads. Taps may be straight flute or spiral flute, depending on the material and hole type.
- Thread Milling: Offers superior precision, reduces tool breakage, and works well for hard or large-diameter holes.
- Thread Forming: Produces threads by displacing material instead of cutting, resulting in strong threads without chip production.
Applications of Threaded Holes

Threaded holes are essential in nearly every sector:
- Automotive: Engine blocks, gear housings, and structural components.
- Aerospace: Lightweight alloys tapped for secure and vibration-resistant fasteners.
- Tooling & Molds: Dies, jigs, and molds often contain precision internal threads.
- Electronics: Fastening components on circuit boards and device enclosures.
- Construction Machinery: Heavy-duty threaded holes for bolts and structural assemblies
Key Factors for High-Quality Threaded Holes
- Correct Pilot Hole Size & Tap Selection: Crucial for thread strength and tap longevity.
- Material Considerations: Hard steel, aluminum, plastics, and composites require tailored techniques.
- Lubrication & Cooling: Helps reduce friction, extend tool life, and produce smoother threads.
- Thread Depth & Engagement: Proper depth ensures reliable fastening.
- Machine Stability & Alignment: Prevents misaligned or skewed threads.
Common Problems and How to Fix Them
- Stripped Threads: Usually caused by incorrect drill size or overtightening. Solution: Follow tap drill size charts and recommended torque limits.
- Broken Taps: Often occurs with hard materials or improper lubrication. Solution: Use spiral taps, proper cutting fluids, and reduce feed rates.
- Oversized or Undersized Threads: May result from worn tools or inaccurate pilot holes. Solution: Inspect taps regularly and replace when needed.
- Poor Surface Finish or Misalignment: Can compromise fastener engagement. Solution: Ensure machine rigidity, correct alignment, and use quality taps or thread mills.
Best Practices for Threaded Holes
- Choose appropriate tap or thread mill material: HSS, cobalt, or carbide depending on material hardness.
- Use cutting fluids or lubrication to protect tools and produce smooth threads.
- For precision or large-diameter holes, consider CNC thread milling.
- Always follow industry tap and drill size charts.
- Maintain proper machine setup and alignment to prevent angled or damaged threads.
Why Choose Shixinproto for Threaded Hole Machining
A threaded hole might seem simple, but producing high-quality internal threads requires expertise, precision, and the right tools. At Shixinproto, we specialize in precision threaded hole machining, delivering reliable, durable, and accurate threads for a wide range of industries — from automotive and aerospace to electronics and tooling. By leveraging advanced CNC machines, high-quality taps and thread mills, and industry best practices, Shixinproto ensures every threaded hole meets your exact specifications.
With our commitment to quality, precision, and efficiency, Shixinproto helps manufacturers achieve stronger assemblies and consistent results — keeping your components secure and performing at their best.