
If you’ve ever wondered how turbine blades in a jet engine stay cool at extreme temperatures or how medical instruments contain perfectly smooth micro holes, the answer often lies in small hole EDM (Electrical Discharge Machining). This specialized machining process is one of the quiet heroes of precision manufacturing—capable of drilling ultra-fine, deep holes that traditional methods can’t handle.
Understanding the Basics of Small Hole EDM
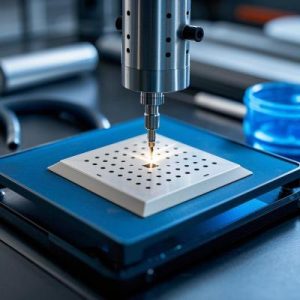
Small hole EDM, sometimes called micro EDM drilling, is a non-traditional machining process that removes material using controlled electrical discharges rather than physical contact. A rotating copper or brass tube electrode generates thousands of tiny sparks between itself and the workpiece, vaporizing material to form a precisely shaped hole.
The dielectric fluid—typically deionized water—cools the gap and flushes away debris. Because there’s no mechanical pressure or tool contact, small hole EDM eliminates burrs, tool breakage, and surface deformation. This makes it ideal for machining hard, conductive materials like tungsten carbide, titanium, and Inconel.

Why Manufacturers Choose Small Hole EDM
Traditional drilling and laser machining both have limits when it comes to micro hole drilling. Mechanical drills struggle with tool wear and deflection, especially in deep, narrow geometries. Lasers can achieve smaller holes, but they often create heat-affected zones or leave rough edges that require post-processing.
Small hole EDM overcomes these challenges with:
- Exceptional accuracy: Achievable tolerances within a few microns
- High aspect ratios: Depth-to-diameter ratios up to 100:1
- No thermal distortion: Minimal heat input, perfect for delicate components
- Material versatility: Works with any conductive metal, regardless of hardness
In short, it’s the go-to solution when precision and surface integrity matter more than raw speed.
Key Process Parameters for Precision Results
Achieving the best results with EDM hole drilling machines depends on tuning several parameters:
- Discharge current and voltage: Control the energy released per spark, influencing material removal rate
- Pulse on/off time: Affects surface finish and electrode wear
- Electrode rotation speed: Enhances flushing and maintains roundness
- Dielectric pressure: Helps clear debris, especially in deep or blind holes
Modern CNC-controlled EDM systems automatically adjust these variables to maintain optimal stability during machining.
Real-World Applications

The range of industries using small hole electrical discharge machining continues to expand as demand for micro precision grows:
- Aerospace: Drilling cooling holes in turbine blades, fuel injector orifices, and engine components. For example, manufacturers like GE and Rolls-Royce use EDM drilling to ensure uniform cooling and improved efficiency in jet turbines.
- Medical: Producing micro holes in surgical instruments, hypodermic needles, and implant components where cleanliness and accuracy are critical.
- Automotive: Creating precision injector holes and sensor ports for modern fuel systems.
- Tool and Mold Making: Adding venting or lubrication channels in molds without damaging the surrounding surfaces.
In each case, EDM’s non-contact nature allows engineers to work with complex geometries that mechanical tools simply cannot reach.
Practical Insights from the Shop Floor
Engineers often face real-world challenges during small hole EDM—like electrode wear, misalignment, or inconsistent flushing in deep holes. Experienced machinists overcome these by:
- Using shorter electrodes for pilot holes before deep drilling
- Monitoring dielectric purity to avoid unstable discharges
- Regularly compensating for electrode wear in the CNC program
Such practical know-how is what turns good EDM results into repeatable, production-grade performance.
Conclusion
Though it often works quietly behind the scenes, small hole EDM plays a critical role in shaping the future of precision manufacturing. Whether it’s cooling systems in aircraft engines, micro channels in medical tools, or high-performance molds, this process delivers the accuracy and reliability that modern industries demand.
As automation and intelligent control continue to advance, small hole EDM drilling will remain an indispensable technology—pushing the boundaries of what’s possible in micro-scale engineering.