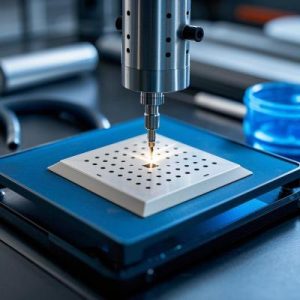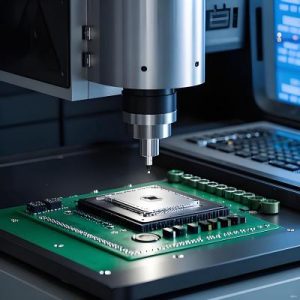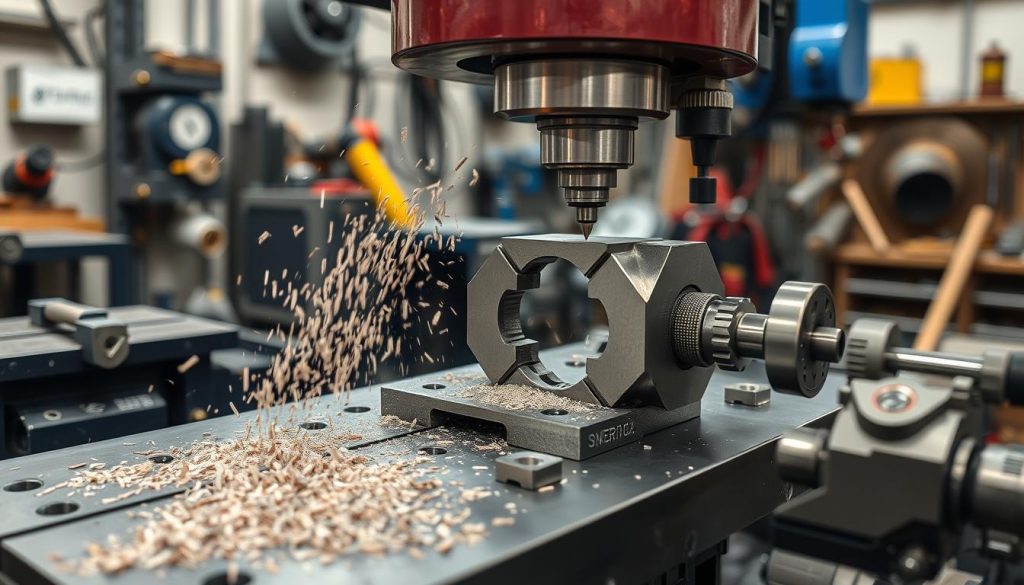

Pocket milling is one of the most widely used operations in CNC machining, essential for creating cavities, recesses, and internal features found in nearly every machined component. From precision housings to mold bases and mounting features, pocket milling enables efficient material removal while maintaining accuracy and surface quality.
In this guide, we’ll break down what pocket milling is, how it works, the best tooling options, and practical strategies you can use to improve machining performance.
What Is Pocket Milling?

Pocket milling refers to the removal of material inside a closed boundary to create a recessed area. These pockets can be shallow, deep, open-ended, or fully enclosed, and can vary from simple rectangles to complex 3D forms.
Pocket milling is common in parts requiring:
- Weight reduction
- Internal cavities
- Mounting seats and slots
- Electronic housings
- Mold and die features
Common Types of Pockets
Different designs require different machining approaches. Some common pocket types include:
Rectangular Pockets
Simple geometry typically found in mechanical components and fixtures.
Circular Pockets
Common for bearing seats, counterbores, or clearance features.
Irregular or Freeform Pockets
Used in molds, aerospace components, and complex parts.
Deep Pockets
Require optimized toolpaths and rigid setups to maintain accuracy.
Tools for Pocket Milling
Selecting the right tool improves efficiency and surface quality.
Flat End Mills
Ideal for roughing and finishing flat-bottom pockets.
Corner Radius End Mills
Increase tool strength and reduce wear in high-load cutting.
High-Efficiency End Mills
Designed for high-speed machining and improved chip evacuation.
Roughing (Hogging) End Mills
Useful for quickly removing large amounts of material.
Tool Selection Tips
- Use larger tools to maximize roughing efficiency
- Choose corner-radius tools for deeper pockets
- Opt for coatings like TiAlN when machining hardened materials
Pocket Milling Strategies
Choosing the right strategy depends on pocket geometry, material, and accuracy requirements.
Traditional Offset Toolpaths
A simple method using concentric offsets. Effective for basic pockets but can cause uneven chip loads.
Adaptive Clearing (High-Efficiency Milling)
Modern CAM systems use constant tool engagement to maximize material removal.
Benefits include:
- Higher feed rates
- Reduced tool wear
- Better heat management
- Improved chip evacuation
Zigzag or Raster Machining
Ideal for long, narrow pockets where directional passes are efficient.
Helical or Ramp Entry
Safer than plunge-cutting and improves flute life.
Key Parameters for Pocket Milling
Step-Over
Affects scallop height and machining time. Smaller step-overs produce smoother surfaces.
Step-Down
Controls axial load. Deeper step-downs can be used with high-efficiency toolpaths.
Cutting Direction
Climb milling provides better finish and lower tool wear.
Speeds and Feeds
Higher feed rates are possible when using adaptive clearing strategies.
Common Pocket Milling Applications

Pocket milling is used across a wide range of industries and part types. Some typical applications include:
- Mechanical Components: Internal slots, recesses, and cavities in brackets, housings, and gearboxes.
- Mold and Die Making: Creating cavities for injection molds, die sets, and stamping tools.
- Electronics Enclosures: Recesses for PCBs, connectors, and mounting features.
- Aerospace Components: Lightweight pockets for structural parts while maintaining strength.
- Automotive Parts: Engine components, transmission housings, and other internal cavities.
Understanding these common uses helps in selecting the appropriate tool, strategy, and CAM setup for efficient pocket milling.
Common Issues and Solutions
Chatter
Reduce tool overhang, increase feed, or use more rigid tooling.
Poor Floor Finish
Use a dedicated finishing pass with a small step-over.
Tool Breakage
Reduce axial load or switch to adaptive toolpaths.
Inconsistent Pocket Depth
Check machine calibration and ensure proper tool length setting.
Advanced Pocket Milling Techniques
- Use rest machining to clean tight areas after roughing
- Combine large- and small-diameter tools for hybrid efficiency
- Employ trochoidal toolpaths for hard materials
- Use chamfer tools to break edges after finishing
Conclusion
Pocket milling is a core CNC machining operation that allows efficient creation of internal features across countless applications. With the right toolpaths, tooling, and setup, you can significantly improve machining speed, surface finish, and tool life.
Whether you’re roughing deep cavities or finishing tight clearances, mastering pocket milling techniques will help you produce better parts with fewer machining challenges.